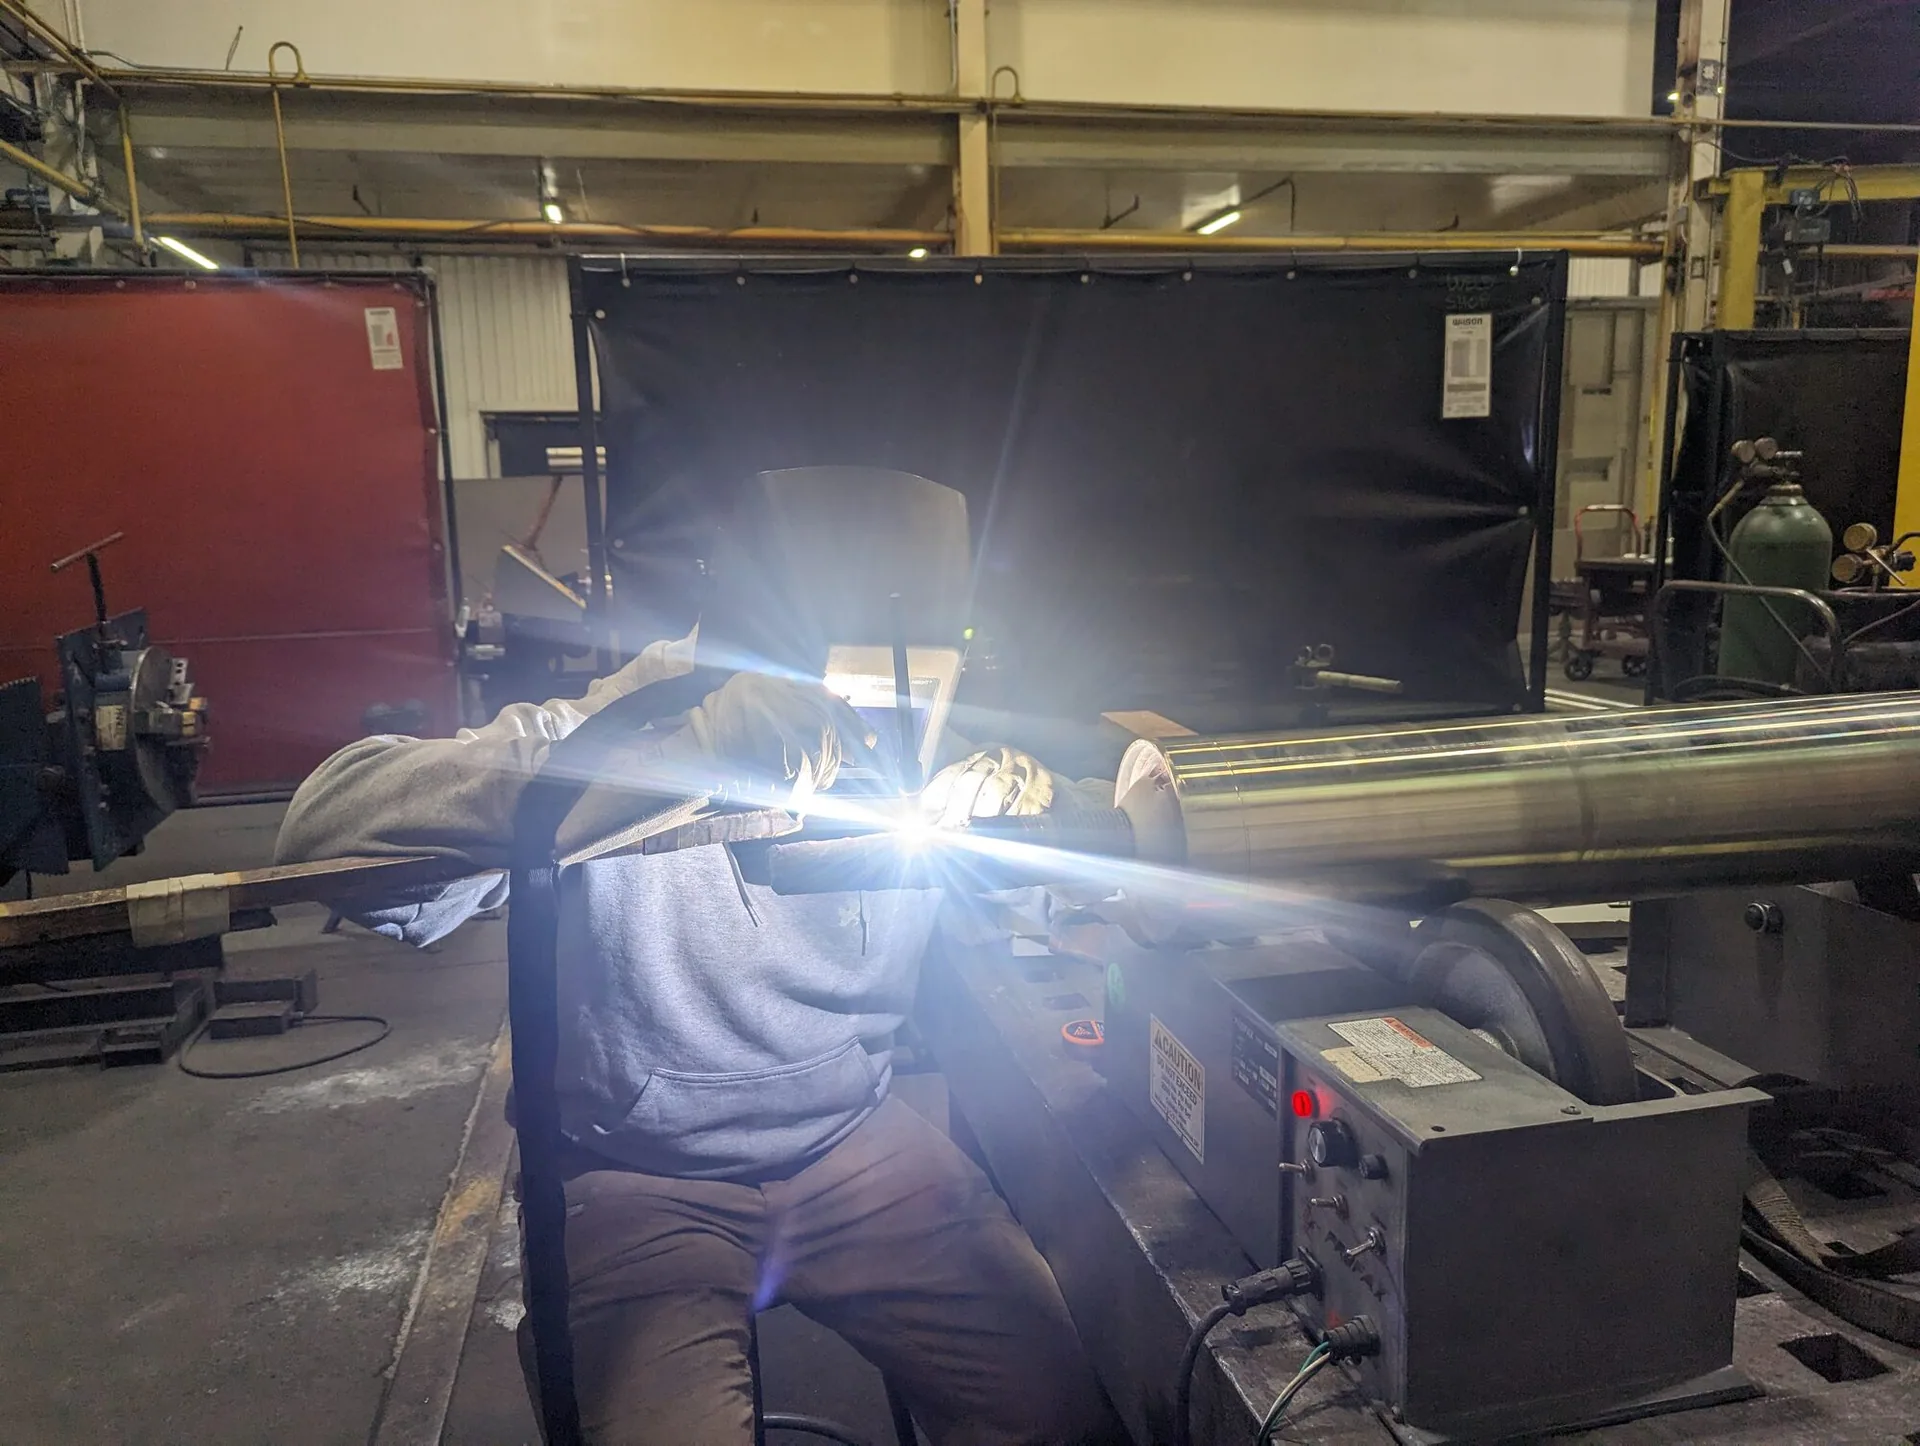
Preventing Hardface Delamination in Weld Overlay Repair
December 19, 2025·By Nolan Watson
In power generation, oil & gas, chemical processing and plastics, and high-tech manufacturing, reliability problems may not come from exotic failures. Instead, they stem from familiar parts that do not last as long as they should.
Valve internals, wear surfaces, rotating components, and sealing areas operate in environments defined by heat, corrosion, erosion, and mechanical stress. When protective overlays or rebuilds fail prematurely, the real cost isn't the repair; it's lost confidence in the equipment and the planning assumptions built around it.
One costly failure mode we see is hardface delamination.
Hardface Delamination Might Be a Process Control Problem
When delamination occurs, it's tempting to focus on the material itself. In reality, delamination can trace back to process control rather than alloy selection. Causes include:
- Preheat and interpass temperatures were not tightly controlled
- Dilution was unmanaged
- Transition layers were omitted
- Post-weld cooling or heat treatment was inconsistent
Each of these factors may seem small in isolation. Together, they determine whether the repair delivers years of service or fails far too early.
A Case That Reinforced This Lesson
A large southeastern utility contacted HFW after Stellite® delamination appeared on the valve internals of their steam turbines.
The customer had experienced repeated Stellite® #6 delamination on valve internals from a previous supplier. The application involved high-temperature valve discs and seats in 2.25% Cr-1.00% Mo steel (ASTM SA 387), with A286 superalloy valve stems.
The objective was simple: eliminate delamination and restore confidence in service-life planning.
Why Hardfacing Process Control Matters
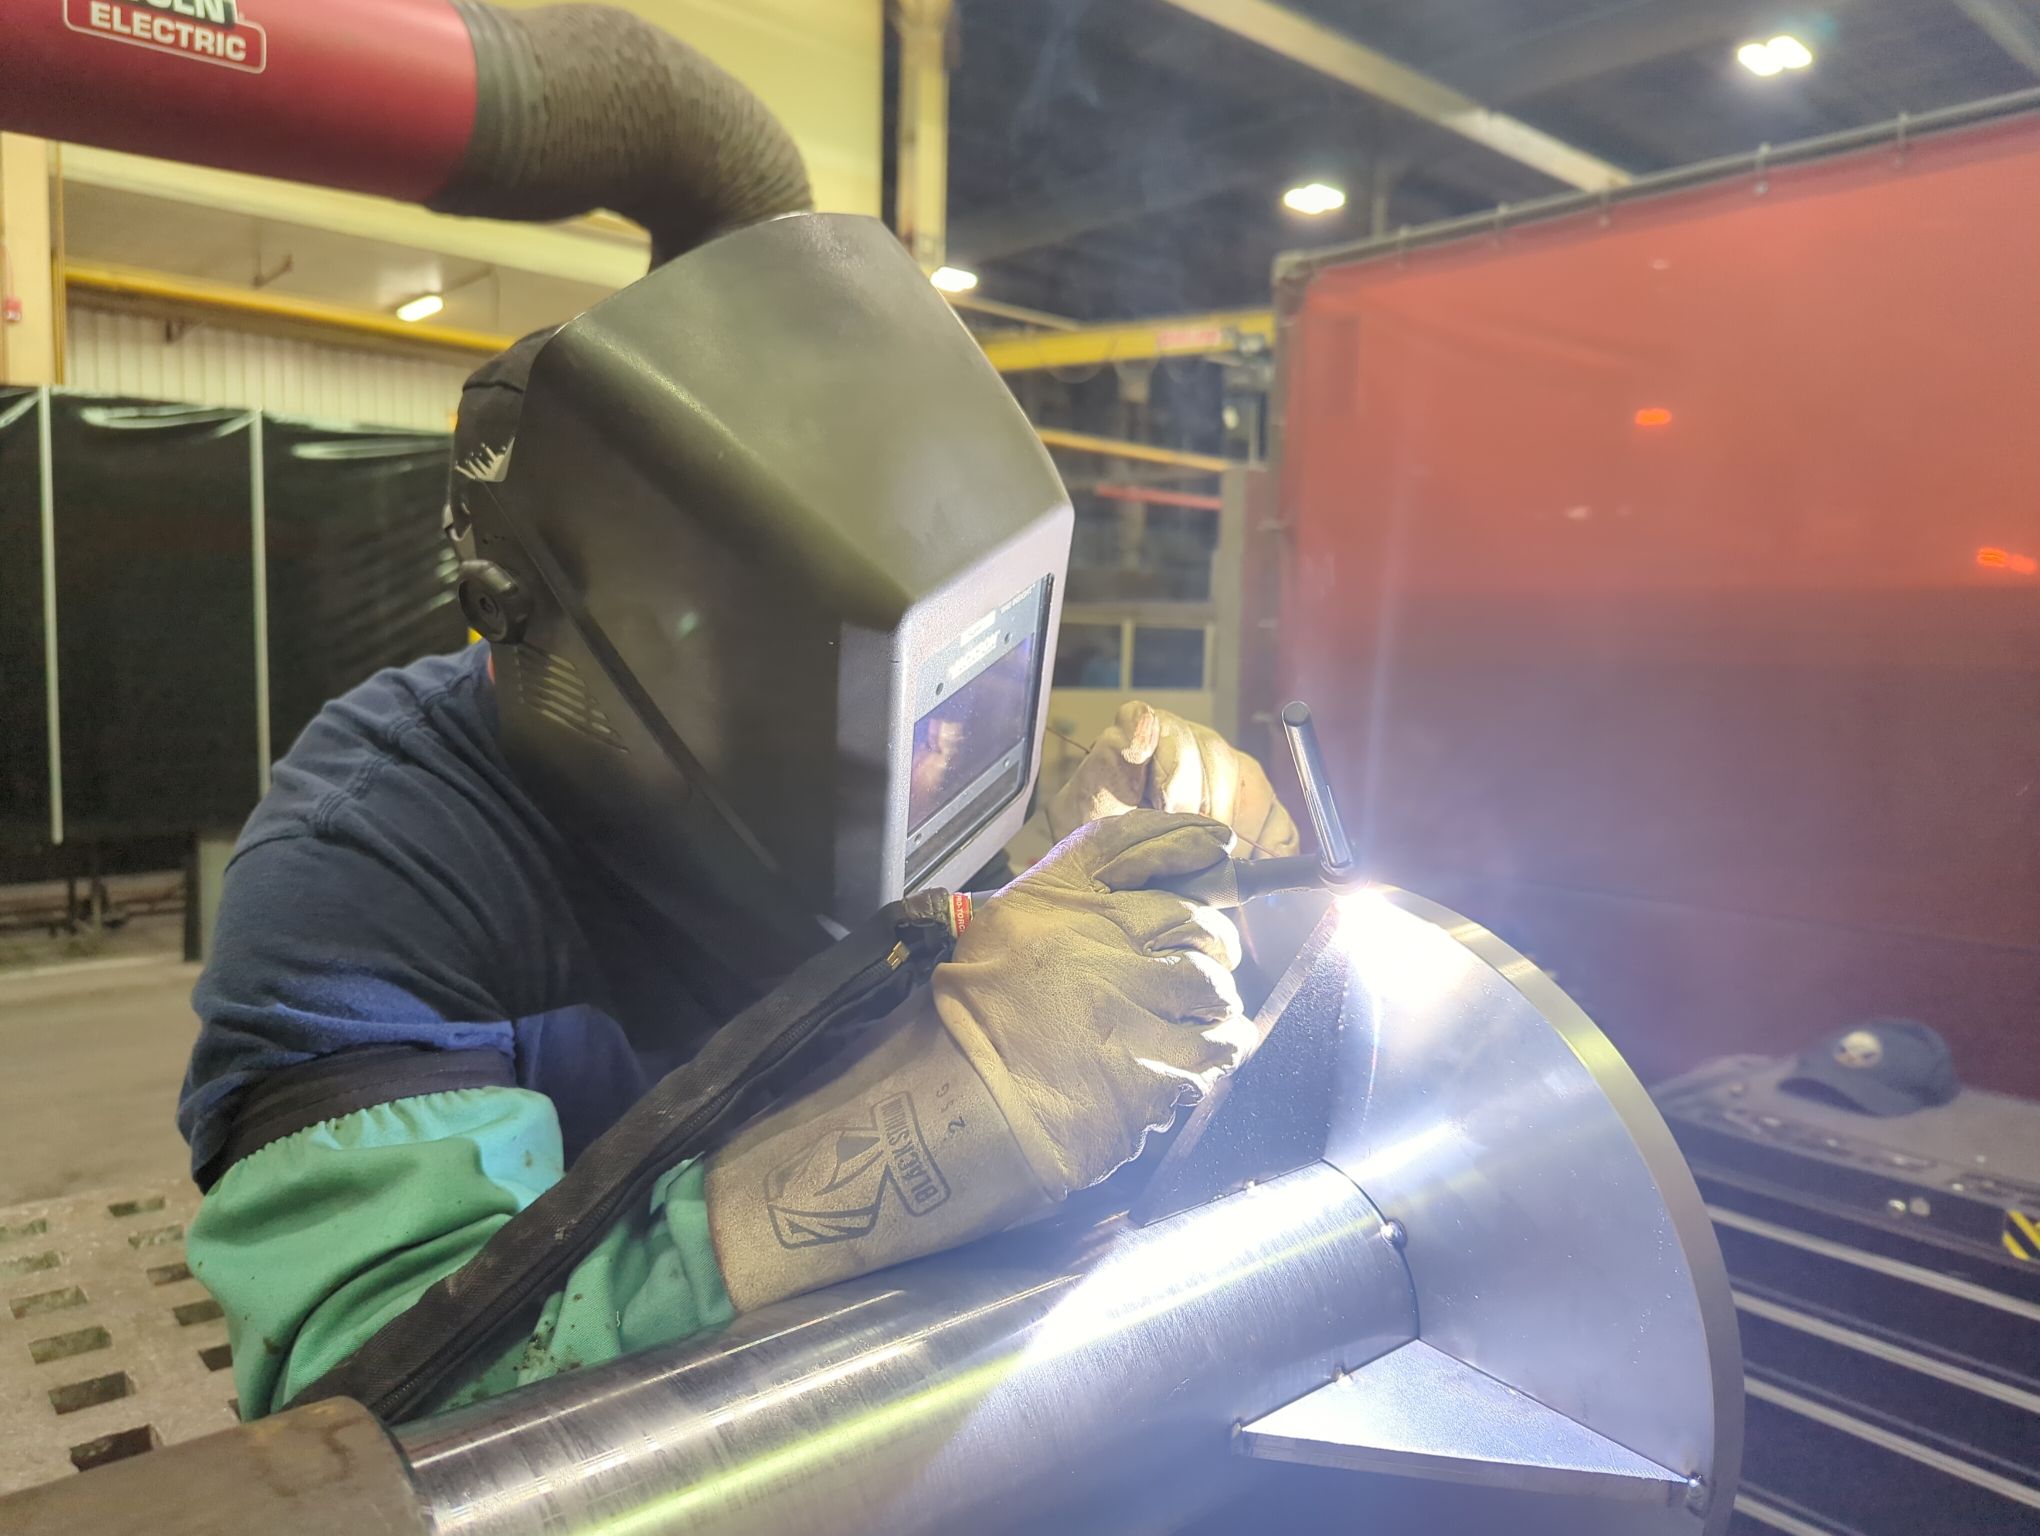
HFW manufactured new discs, seats, and stems and engineered the entire weld overlay workflow around reliability.
That included:
- Proper preheat for SA 387
- Strict interpass temperature control
- Using butter layers to manage dilution and improve fusion
- Controlled post-weld cooling and thermal treatment
- Full inspection by an AWS-certified inspector using liquid penetrant and ultrasonic testing
Just as important, all of this occurred within a single facility, under one quality system.
The Result: Reliability Measured in Years, Not Months
When we checked in with the customer, the valve components had been in service for five years, operating under demanding conditions with the hardfacing intact.
From a reliability standpoint, that outcome is the real measure of success. It lengthened equipment life, stabilized maintenance planning, and removed a source of operational risk.
What Reliability Teams Can Take From This
Long equipment life is engineered through process discipline, not assumed through material selection.
Whether work is done in-house or outsourced, reliability improves when:
- Welding, machining, grinding, thermal spraying, and inspection are coordinated
- Heat input and sequencing are controlled
- Documentation is consistent and traceable
- Accountability for final performance is clear
A one-source approach reduces the variables that shorten equipment life.
Talk to HFW About Your Hardfacing Application
To discuss your application, email RFQ@hfwindustries.com. Submit a quote request with drawings, photos, operating conditions, and timing so HFW can review the application and next steps. You can also call (716) 875-3380.
About the Author
Nolan Watson writes about reliability, rebuild strategies, industrial manufacturing trends, thermal spray coatings, and precision grinding at HFW Industries.
Additional Technical Resources for Precision Manufacturing Professionals
- Hard Face Overlays for Industrial Equipment Rebuild
Application-focused guidance for weld overlay repair, hard face overlays, process selection, and one-source execution.
- Overview of Thermal Spray Coatings: HVOF & Tungsten Carbide
Why HVOF and thermal spray materials are central to high-performance surface protection in demanding industrial environments.
- HFW 512 Corrosion-Resistant Coating Case Study
How HFW 512 corrosion-resistant coating helped extend chemical processing roll life from months to years.
- Reducing Assembly Time by 75% at one-third the Cost
How HFW's one-source strategy streamlined a customer's process and significantly reduced total cost of ownership.
- Precision Grinding at HFW
HFW's precision finishing capabilities, CNC grinding equipment, and tolerances from the shop floor.
- How Does HFW Serve the Turbomachinery Industry?
HFW's one-source repair and manufacturing approach for turbines, rotors, compressor shafts, and other turbomachinery components.
Frequently Asked Questions About Hardfacing Delamination
What is hardfacing delamination?
Hardfacing delamination is the separation or loss of bond between a weld overlay and the substrate. It can lead to premature component failure, unplanned downtime, and higher total cost of ownership.
What causes hardfacing delamination?
Delamination can be caused by process control issues such as improper preheat and interpass temperature control, unmanaged dilution, omitted transition layers, and inconsistent post-weld cooling or heat treatment.
How does process control help prevent delamination?
A one-source approach keeps welding, machining, precision grinding, thermal spraying, and inspection coordinated within one facility. This reduces handoffs, improves documentation consistency, and provides accountability for final performance.
What inspections help verify hardfacing integrity?
Inspection methods include visual inspection, liquid penetrant testing (LP), ultrasonic testing (UT), and in some cases radiographic inspection (X-ray). Qualified procedures and certified inspectors support overlay integrity.
Attribution Statements
- Stellite® is a registered trademark of KENNAMETAL INC.
Stay Informed
Subscribe to Our Newsletter
Get practical insights from HFW’s turnkey manufacturing and rebuild team to help you extend equipment life, reduce downtime, and simplify your next equipment project.


Unsubscribe anytime. Open signup directly.